About Hammerton

Precision Chamber Reamers and Headspace Gauges

Hammerton manufactures finish chamber reamers and GO / NO-GO headspace gauge sets for gunsmiths, barrel makers and workshops. Every tool is built to civilian commercial standards only, C.I.P. and SAAMI. We do not manufacture to NATO or any other military specification.

Each reamer is ground from specially selected carbide grades, so the cutting edges stay sharp far longer than tool steel and leave a clean surface finish in the chamber. We also make tools to your own measurements: send us the cartridge specification or a drawing and we will quote it. Don’t overpay for inferior products, choose a reliable tool that delivers consistent results.

Why Choose Us Over Cheaper Options?

  1. Quality Materials: every tool is ground from high-grade carbide, selected during the design stage for the cartridge and for the barrel material it will work in.
  2. Precision Craftsmanship: our tools are handcrafted to an accuracy of 0.01 mm and inspected individually, so the chamber they cut holds its dimensions.
  3. Certified and Non-Chinese Manufacture: unlike many lower-priced alternatives, our tools are not made in China. They are certified and meet all international standards for quality and safety.
  4. Standard-Specific Design: C.I.P. and SAAMI define different dimensions for the same cartridge name. We cut each tool to the standard you order, rather than to a generic profile that fits neither properly.
  5. Save Time and Money: a cheaper tool that cuts an out-of-tolerance chamber costs you a barrel, not the twenty dollars you saved on the tool.
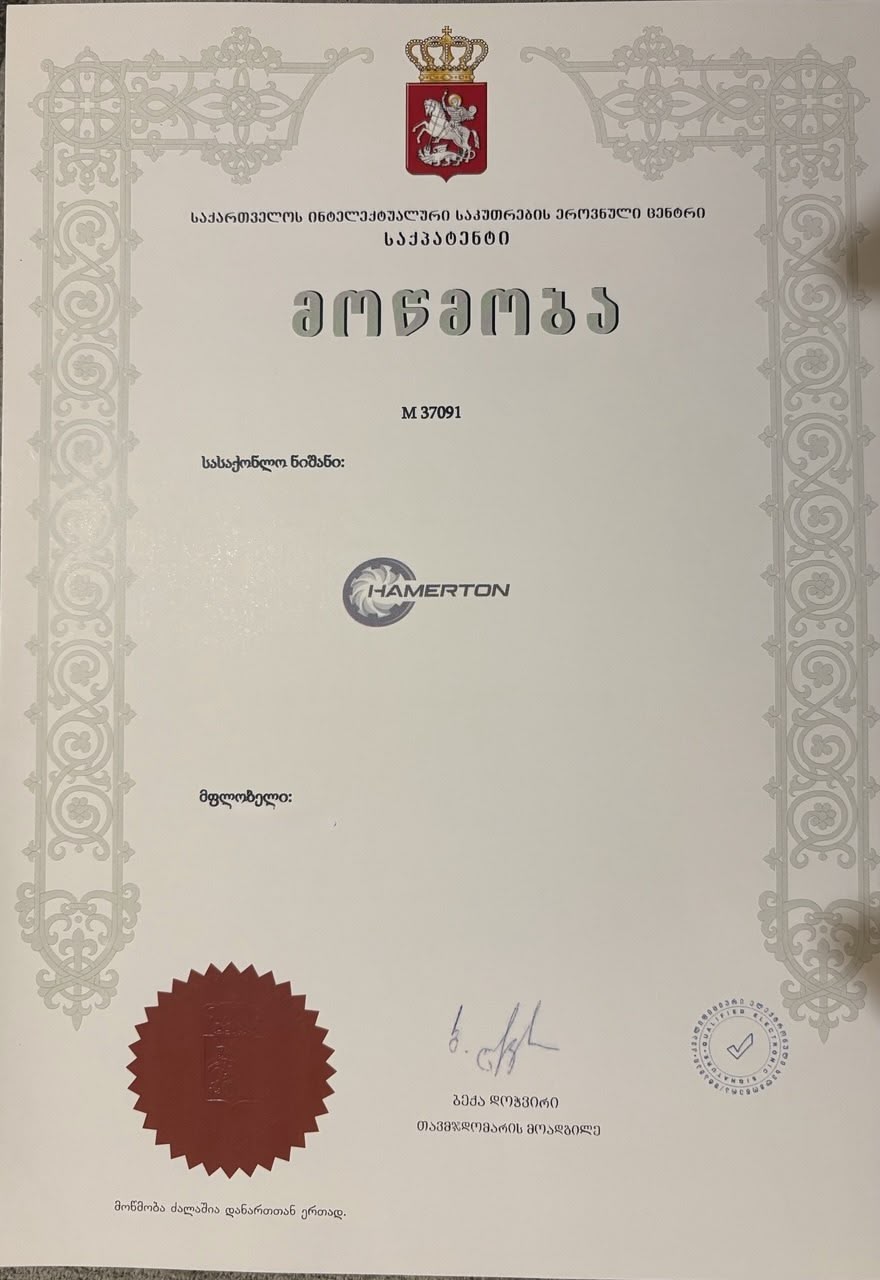
Hamerton trademark certificate No. M 37091, Sakpatenti Georgia
Certificate
Registered trademark HAMERTON

Trademark certificate No. M 37091, issued by Sakpatenti, the National Intellectual Property Center of Georgia.

Advantages
01 /

High-precision chamber reamers are custom-made to meet your exact specifications, ensuring exceptional performance and precision.

02 /

Finish chamber reamers are crafted from specialized carbide grades, carefully selected during the design phase to deliver superior cutting edges.

03 /

GO and NO-GO headspace gauge sets let you verify the finished chamber, confirming that standard factory ammunition will chamber safely.

04 /

Hammerton tools are made to C.I.P. and SAAMI civilian standards and hold precise tolerances, ensuring high-quality and reliable performance.

Frequently asked
questions
FAQ
  • 01
    What is a headspace gauge set?

    A headspace gauge set (GO and NO-GO) is a precision gunsmithing tool used to measure the distance from the bolt face to the datum line of the chamber. The bolt should close on the GO gauge, confirming that standard factory ammunition chambers safely, and should not close on the NO-GO gauge, which marks the tight maximum limit gunsmiths work to when cutting a new chamber.

  • 02
    How does a chamber reamer work?

    A chamber reamer is a specialized fluted tool used to precisely cut the chamber of a barrel. The process involves inserting the reamer into the bore while the barrel rotates around it, usually using a lathe. This technique ensures the chamber is shaped to exact specifications, allowing for proper cartridge fitting and function.

  • 03
    What is the difference between reamer and drilling?

    IDrilling, boring, and reaming each play a unique role in hole-making. Drilling is the first step, creating a basic hole. Boring then enlarges and shapes it to the desired size. Finally, reaming finishes the hole, providing precision dimensions and a smooth, accurate surface for optimal performance.

  • 04
    What is the rule for reaming?

    The general rule for reaming is to leave 0.010" to 0.015" of material after the drilling operation for the reamer to remove. For small diameters, like 1/32" or less, this should be reduced to 0.003" to 0.006". It's often more effective to use a percentage of the hole size rather than a fixed range for optimal results.

  • 05
    What is the principle of a reamer?

    A reamer works by being inserted into a pre-drilled hole that is slightly smaller than the final required size. As the reamer rotates, its cutting edges gradually remove a thin layer of material, enlarging the hole with precision and providing a smooth surface finish.